
Inconel, titanium and duplex welding in Vista, CA
Nickel alloy, titanium and duplex parts are expensive to scrap, and the paperwork has to show the weld was done right. We TIG weld all three to a written procedure qualified for your job, and ship the parts with material certs and test results.
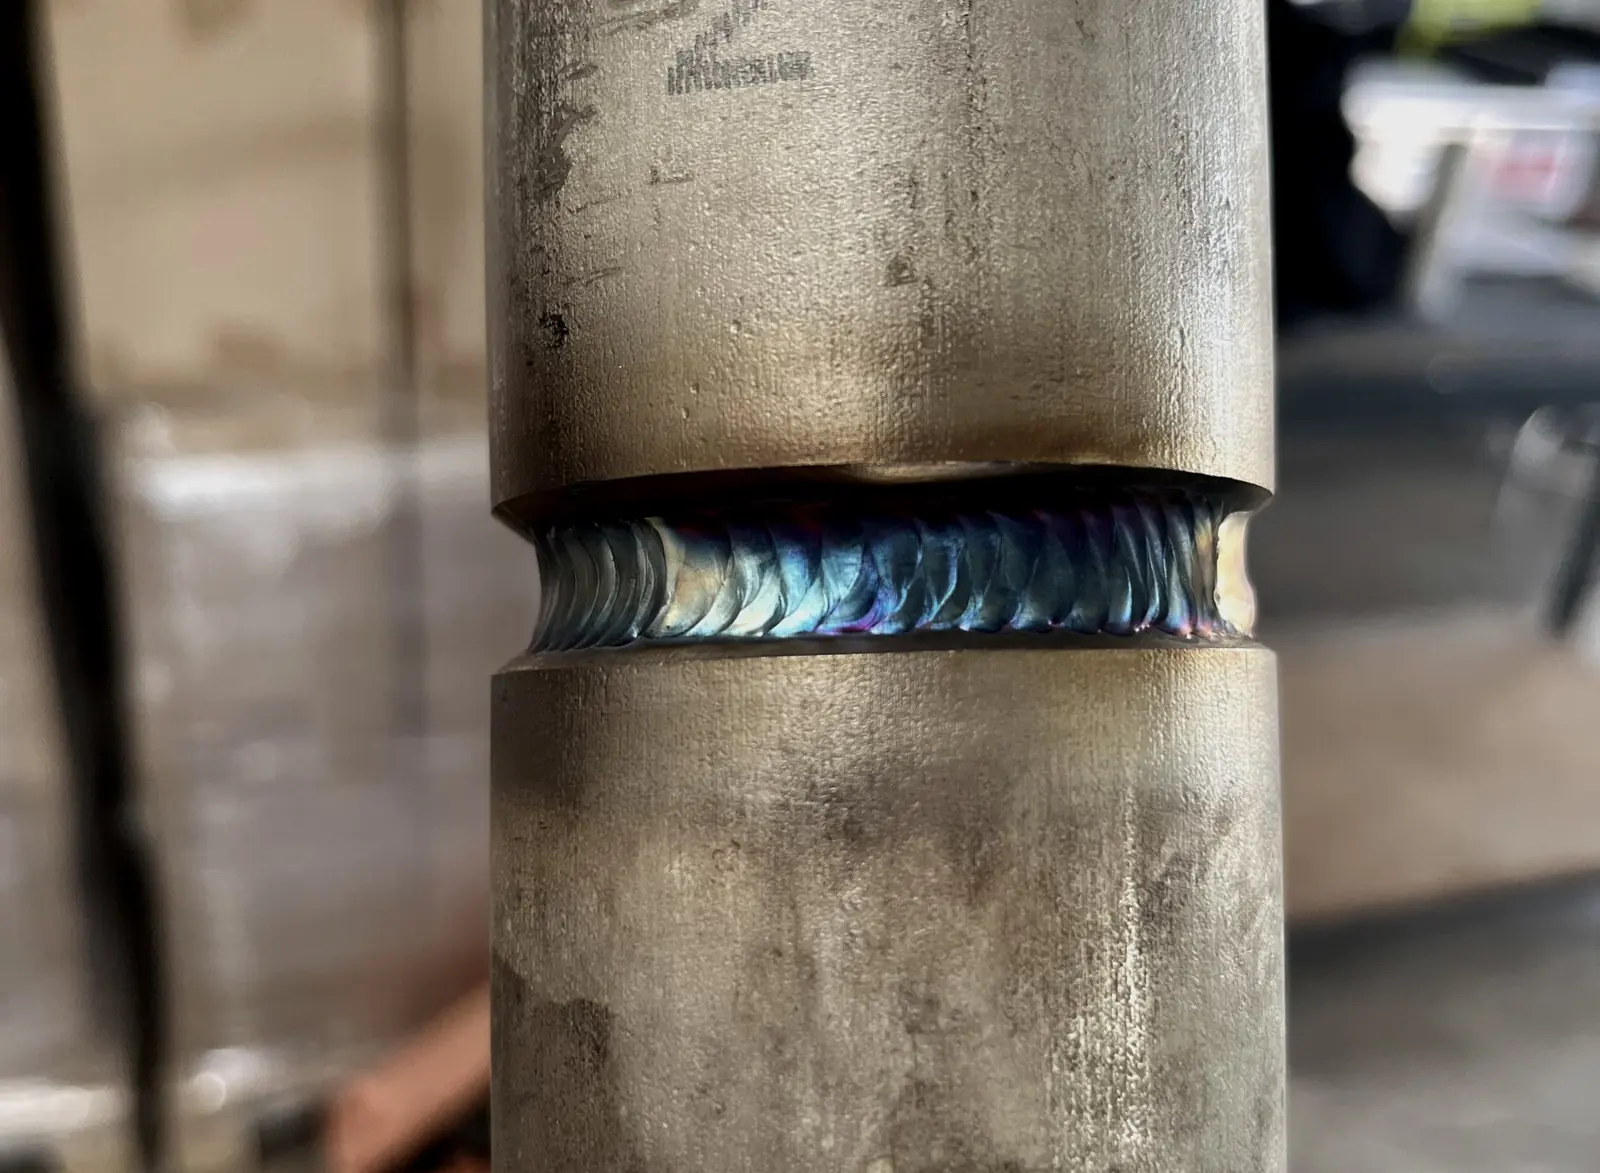
What we weld in these alloys.
Parts built to your drawing, one prototype or a production run.
Inconel and other nickel alloys
TIG welded to a procedure written for the alloy and the joint, with the filler your spec calls for.
Titanium
TIG welded with the gas shielding titanium needs. Weld color is part of the visual inspection.
Duplex stainless
TIG welded with heat input held to the procedure, which is what keeps duplex’s ferrite-austenite balance in range.
What to tell us when you quote an alloy job.
- The exact alloy or grade.
- “Inconel” covers several nickel alloys, and titanium comes in several grades. The procedure and filler depend on which one, so put it on the drawing.
- The code or spec.
- AWS D1.6, ASME Section IX, ASME B31.3 or your customer’s spec. We qualify to what your job calls for.
- The acceptance criteria.
- Weld color limits, dye penetrant (PT), or X-ray and ultrasonic. PT is in-house. RT and UT go through an independent lab when required.
- The finish.
- Passivation for duplex, or post-weld machining, done in-house or through our finishing partners.
Capabilities
Alloy welding capabilities.
Materials, procedures, testing and paperwork for nickel alloy, titanium and duplex work.
| Materials | Nickel alloys (Inconel) · titanium · duplex stainlessAlso stainless (including 316), aluminum and carbon steel. |
|---|---|
| Process | TIG (GTAW) |
| Codes | AWS D1.6 · ASME Section IX · ASME B31.3Other codes on request. We qualify to what your job calls for. |
| Procedures | WPS/PQR developed and qualified · welder qualification records |
| Fixtures | Welded steel, 3D-printed or hybrid, built before welding so every part sets up the same |
| Inspection | First part checked against your drawing before the run · visual weld inspection |
| Testing | In-house: visual (VT), bend tests, dye penetrant (PT)X-ray (RT) and ultrasonic (UT) through an independent lab when the job calls for it. |
| Paperwork | Material certs (MTRs) · weld inspection reports · test results |
| Finishing | Passivation · post-weld machiningIn-house or through our finishing partners. |
| Runs | Single prototypes through production |
| Quoting | Send the drawing (PDF, STEP or DXF), quantity and need-by date. Get a written price and a ship date.NDA on request. Expedited runs when you need them. One point of contact from quote to delivery. |
How an alloy job runs.
The same five steps as every job, with the procedure settled first.
- 01
Send the drawing
PDF, STEP or DXF, the quantity, the need-by date, and the alloy and spec. NDA on request.
- 02
Get a price and a ship date
In writing. If material pricing holds up the quote, we tell you right away. Expedited runs when you need them.
- 03
First part checked to print
Part one is welded to the written procedure and checked against your drawing before the run starts.
- 04
The run
Every part sets up in the same fixture, so the last part matches the first.
- 05
Inspected, packed, documented
Visual weld inspection, then packed and shipped with material certs, weld inspection reports and test results when your job needs them.
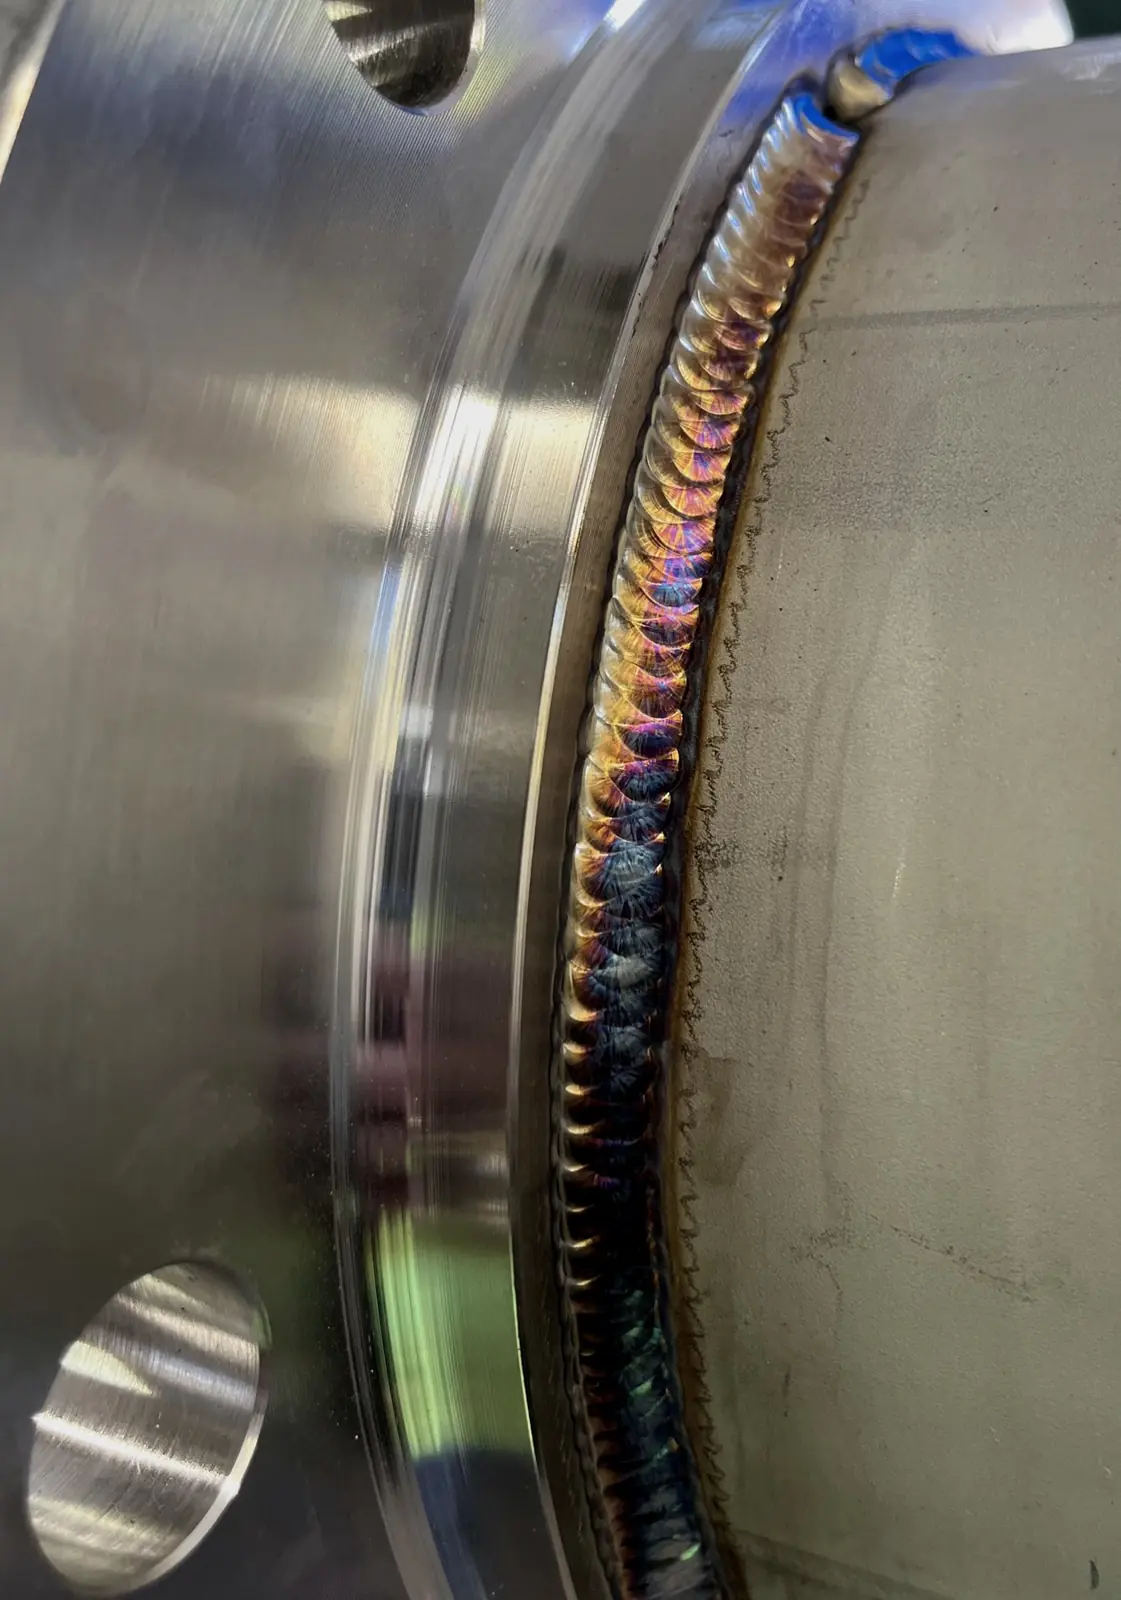
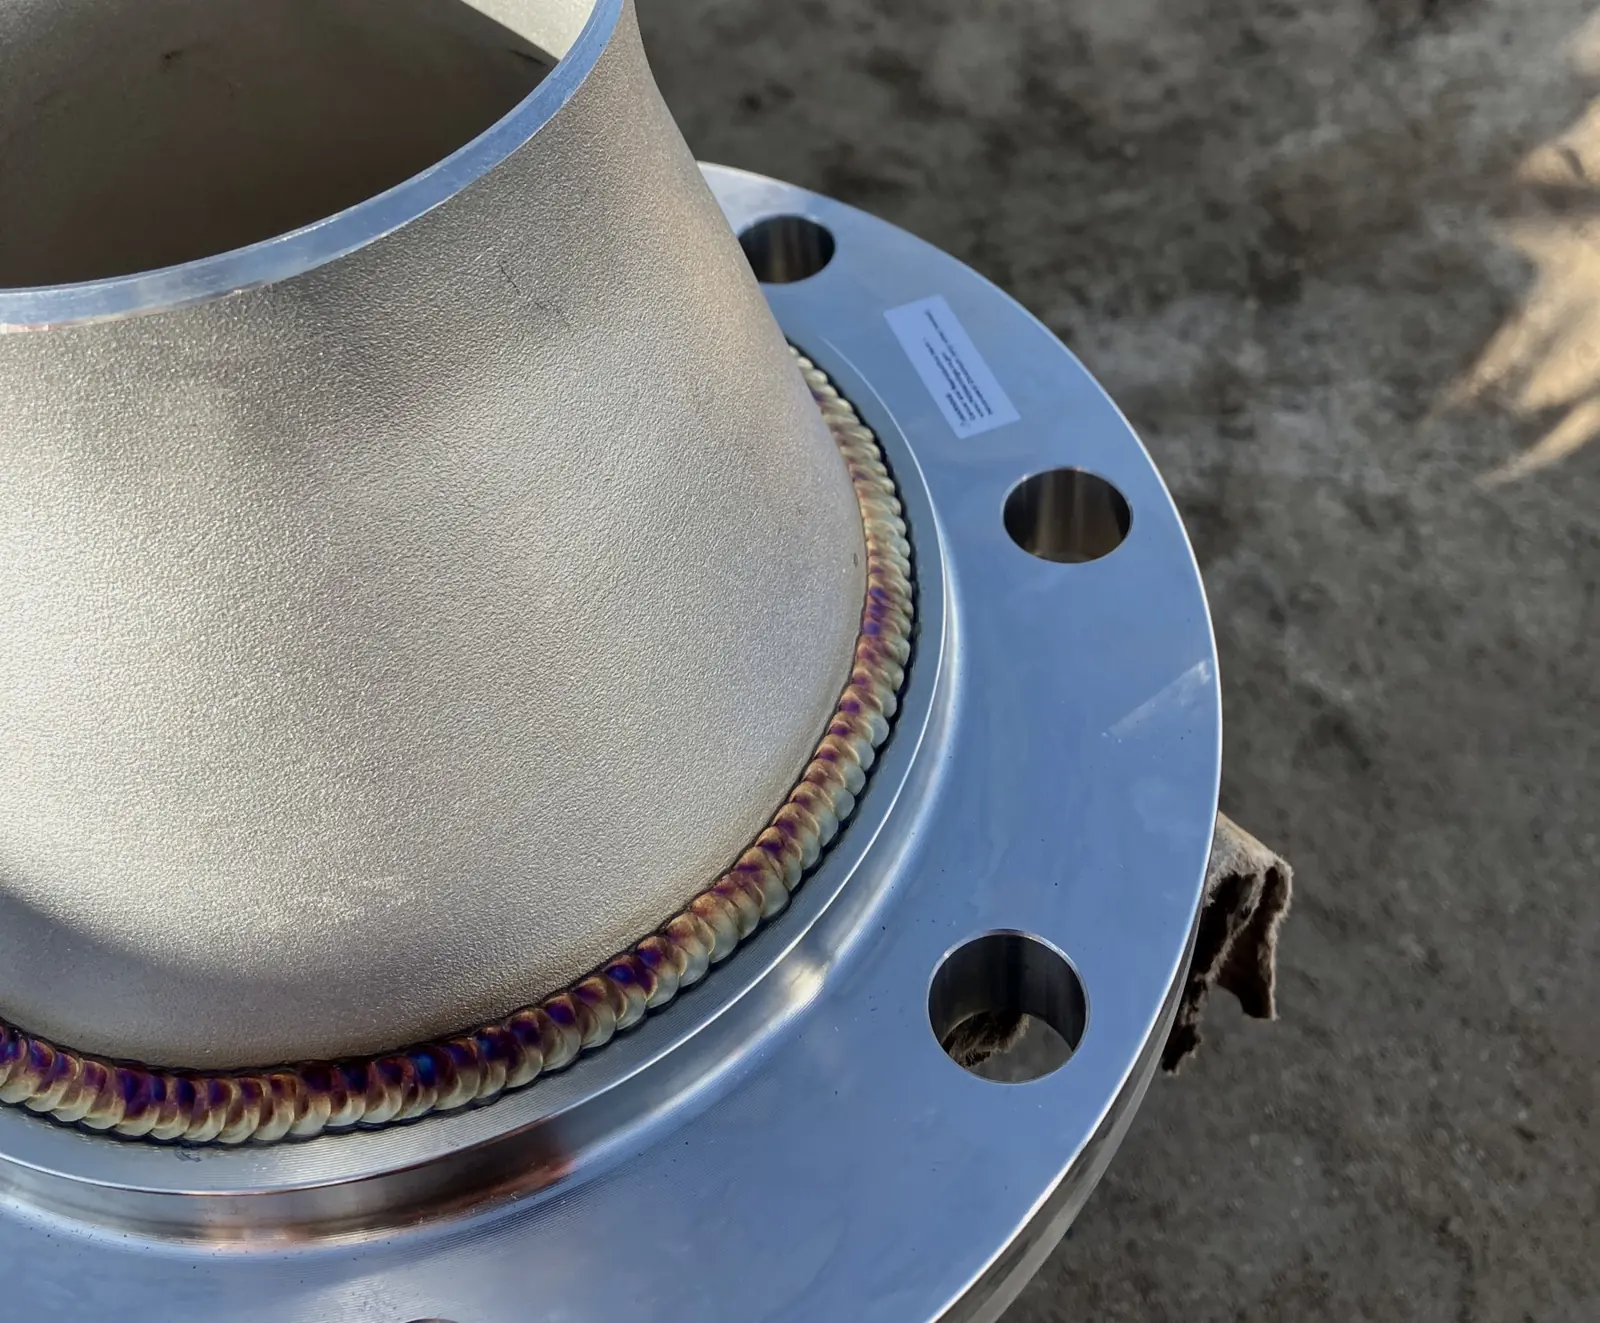
TIG welds from our shop.
These photos show stainless steel TIG welds, not nickel alloy or titanium parts.
Alloy welding questions.
Do you weld Inconel?
Yes. We TIG weld Inconel and other nickel alloys. Put the alloy and spec on your drawing, and we qualify the procedure to what your job calls for.
Do you weld titanium?
Yes, by TIG. Weld color is part of the visual inspection on titanium. Tell us your acceptance criteria and any testing you need.
Can you weld duplex stainless?
Yes. Duplex stainless is TIG welded to a written procedure. Passivation is available in-house or through our finishing partners.
Can you qualify a procedure for our alloy?
Yes. We develop and qualify weld procedures (WPS/PQR) and qualify welders to the code your job calls for. See weld procedures and testing.
What paperwork do we get?
Material certs (MTRs), weld inspection reports and test results, plus the WPS/PQR for code work.
Related
- Stainless steel welding316 TIG welding, heat tint and passivation. AWS D1.6.
- Weld procedures and testingWPS/PQR, welder qualification, VT, bend and PT testing.
- Pipe spool weldingASME B31.3 spools, ASME Section IX procedures, MTRs.
- Prototype to productionFirst part checked to print, then the run.
- Weld in-houseJones Welding Systems, our newest service: cell, fixtures, procedure and operator training.
- Jones Welding & ManufacturingHomepage: parts built in our shop, or welding set up in yours.
Start here
Send us a drawing.
Send the drawing with the alloy or grade, quantity, need-by date and any code or spec. You’ll get a written price and a ship date.
Call(760) 532-8731
Shop
1485 Poinsettia Ave, Suite 106
Vista, CA 92081
Shop visits and supplier audits by appointment